-
Scenario A: Production-ready parts: this is where Fictiv earns the PO
-
Scenario B: Shape-only request or weekend project? A 3D printer for personal use can be enough
-
Scenario C: Oversized, local, or material-heavy requests like laser tube cutting Anoka
-
Scenario D: What if your question is “where are VMC hooks made?”
-
How to tell which scenario you are in
I spent the last five years doing purchasing for a 130-person hardware company. I am not an engineer. I am the person who manages vendors, chases invoices, and occasionally has to explain to finance why the cheapest quote was not actually the right quote.
When I took over purchasing in 2020, my approach was simple: get three quotes, choose the lowest one, call it a win. That approach broke the first time we ordered custom parts. Actually, it broke the first time we ordered custom parts and had to rework them. Since then, I have learned to route the request before comparing prices. Fictiv machining is often the right answer for production-ready parts. A 3D printer for personal use is good for shape tests. And sometimes the local shop behind a search like laser tube cutting Anoka is the right call because the part is too big, too awkward, or too tied to other local work. There is no single source that wins every order.
Scenario A: Production-ready parts: this is where Fictiv earns the PO
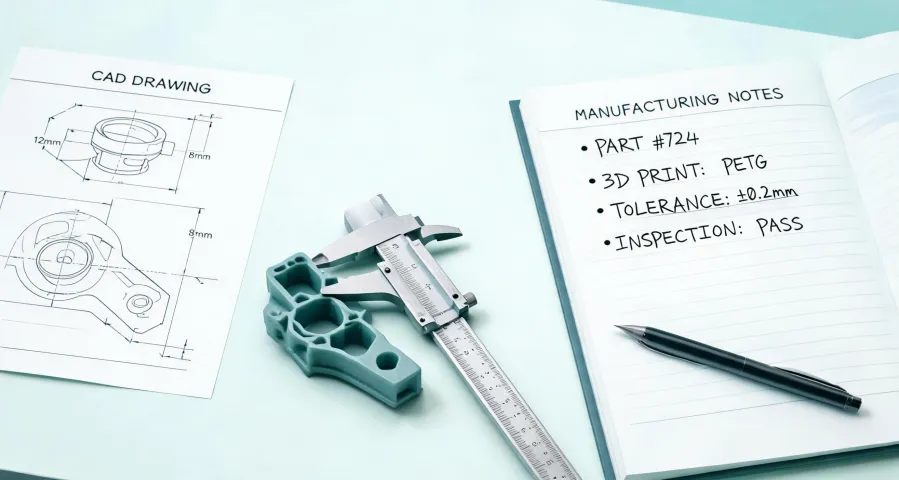
The easiest category is when you already have a CAD model, a material, an expected volume, and the part has to function. Maybe it is a machined bracket for a test fixture. Maybe it is an injection-molded housing that has to survive a drop test. This is the scenario where I use Fictiv digital manufacturing platform.
Fictiv machining is not always the cheapest quote. But the quote is a better starting point because the platform does a design-for-manufacturability check. If the model has a thin wall or an unrealistic tolerance, it gets flagged before the order moves forward. When I first started using Fictiv, I thought DFM feedback was nice-to-have. Then I compared a local quote and a Fictiv quote for the same part. The local quote was lower. It also had no DFM comments, no revision history, and no clear way to reorder the same part later. When the first sample came back wrong, the extra cost went through the roof.
I still kick myself for one order like that. The supplier quoted $740 for a part that Fictiv machining quoted closer to $850. I approved the $740 quote because I was trying to look good to finance. The part came in with a machining issue that the supplier said was “within the drawing,” even though it was not usable in our assembly. The rework cost $620 and cost us five days of development time. That is the difference between a bunch price and total cost.
For Scenario A work, the Fictiv digital manufacturing platform gives me order records, invoice records, and a clean way to approve revisions. If an engineer changes a hole diameter, I can see exactly what changed. That repeatability has real dollar value even when it does not show up on the purchase order.
Scenario B: Shape-only request or weekend project? A 3D printer for personal use can be enough
Not every plastic-looking idea needs to go through a manufacturing platform. If you need one bracket for your garage, or you are not sure whether a handle design fits your hand, get a 3D printer for personal use and test the shape first.
Honestly, the current 3D printers for personal use are better than they get credit for. A desktop printer under $300 can still get you 80% of the way for visual models and simple fit checks. The first versions are supposed to be wrong. That is the point. If I am going to throw away two prototypes, I would rather waste $6 of plastic than $120 of CNC setup.
The mistake I see is choosing a 3D printer for personal use and then trying to make production parts with it. A desktop 3D printed part is not a substitute for CNC aluminum or injection-molded plastic. It has different strength, different heat tolerance, and different surface behavior. For a design conversation, a personal 3D printer is fine. For a structural part, do not force it. That is when I send the file to Fictiv or another proper manufacturing service.
Scenario C: Oversized, local, or material-heavy requests like laser tube cutting Anoka
There is a different kind of job where the local shop makes more sense than any online platform. That is when shipping, part length, or local integration matters more than the DFM review. If a part is a 20-foot steel tube frame, no manufacturing portal is going to handle the freight as smoothly as a local fabricator. If you see a search for laser tube cutting Anoka, that usually means the buyer wants a shop with the equipment and the truck access nearby.
I had this exact situation a while ago. We needed structural steel pieces that were too long for standard parcel shipping. The local fabricator had a fiber laser tube cutter, a forklift, and a relationship with the powder coater down the road. Their quote process was clunky compared to Fictiv’s platform. They sent a PDF invoice and asked for a check. But the total cost was lower because we did not have to arrange freight, coordinate a second inspection, or hope that a 22-foot piece arrived undamaged.
That is the nuance people miss. A local supplier is not automatically worse or less technical. For oversized fabrication, especially something like laser tube cutting Anoka or another local industrial hub, the supplier’s location is part of the product. I still prefer Fictiv machining for standard-size precision parts. But for this scenario, local wins.
Scenario D: What if your question is “where are VMC hooks made?”
This one looks out of place in a manufacturing guide, but it comes up often enough to matter. If your search is where are VMC hooks made, you are not looking for a custom manufacturer. You are trying to verify the origin of a finished, branded product.
VMC is a French hook brand that has been around for a long time. The VMC hooks I have seen in distribution are stamped as made in France, and the company sits under the Rapala VMC umbrella. If you need certainty for import, resale, or quality reasons, check the current package and ask the distributor. Manufacturing locations can change, and old blog posts do not always update quickly.
The reason this matters here is that a product-provenance question and a custom-manufacturing request are two different procurement paths. Do not upload a CAD file for a fishing hook if what you actually need is a purchase order for a standard item. Know whether you are asking “where does this existing product come from” or “can you make a new part for me.”
How to tell which scenario you are in
Here is the quick test I use before pressing send on any RFQ:
- If the part needs to survive real loads, threads, and tight tolerances—use Fictiv machining or another qualified production service. Do not rely on a desktop printer.
- If you are still exploring the shape, or you are making something for personal use—a 3D printer for personal use is enough for the first round.
- If the part is too large, too heavy, or too tangled up with local welding and finishing—look for a local shop. That is the right way to interpret a search like laser tube cutting Anoka.
- If your real question is where a branded product is made, like where are VMC hooks made—check the package, the distributor, or the brand’s official channel before you talk to any machine shop.
The purchasing habit that saved me the most money was not negotiating harder. It was categorizing the request first. Fictiv digital manufacturing platform is now my default for standard precision parts because the process around the quote is worth more than the per-unit price. Local shops still make sense for oversized and regional work. And a 3D printer for personal use will always have a spot in my process because prototypes are supposed to fail early.
If you are making that same decision, do not ask “which supplier is cheapest?” Ask “what kind of problem am I actually solving?” That question will point you to the right tool faster than any spreadsheet of quotes.