-
What should I look for in an aluminum CNC machining service?
-
How do I specify carbon steel forged flanges without getting burned?
-
What separates precision machined components from 'close enough'?
-
Are brass hose nipple connectors as simple as they look?
-
What is the difference between aluminum CNC cutting and aluminum CNC machining?
-
Why does a washing machine Y splitter fail quality checks?
-
Which documentation should I require before approving first delivery?
-
What is the one question most buyers forget to ask?
I am a quality and brand compliance manager at an industrial equipment company. I review every incoming machined component and fitting before it reaches customers—roughly 300 lots a year. In 2024, I rejected 12% of first deliveries because of missing material traceability, dimensional drift, or finish issues. Here are the questions I get from engineers and procurement teams when they source aluminum CNC machining service, carbon steel forged flanges, precision machined components, brass hose nipple connectors, aluminum CNC cutting, and washing machine Y splitters. No fluff. Just the checks I use before I sign off.
- What should I look for in an aluminum CNC machining service?
- How do I specify carbon steel forged flanges without getting burned?
- What separates precision machined components from 'close enough'?
- Are brass hose nipple connectors as simple as they look?
- What is the difference between aluminum CNC cutting and aluminum CNC machining?
- Why does a washing machine Y splitter fail quality checks?
- Which documentation should I require before approving first delivery?
- What is the one question most buyers forget to ask?
What should I look for in an aluminum CNC machining service?
Don’t start with price per part. Start with the process chain: material cert, machining strategy, inspection, finish, packing. For aluminum, alloy matters. 6061-T6 and 7075 behave differently. If the service can’t tell you the temper and lot, that’s a flag. I ask for first article inspection (FAI), material certs, and a clear GD&T read. Tolerance isn’t one number; it’s per feature. When I compared two quotes for the same 6061 bracket—one cheap and vague, one 18% higher with a full inspection plan—I finally understood why the cheaper one had caused three rework loops. The higher quote saved us a week. Fictiv-style platforms can give instant quoting and order management, but instant price doesn’t replace incoming inspection. You still need to verify the first article and spot-check dimensions.
How do I specify carbon steel forged flanges without getting burned?
Write the standard into the PO. For many carbon steel forged flanges, that means ASME B16.5 dimensions, ASTM A105 or A350 material, pressure class, facing type (RF, FF, RTJ), and traceability. Require mill test reports (MTRs) tied to heat numbers. In our Q1 2024 quality audit, we caught a batch where the raised face height was off enough to risk gasket seating. The supplier called it 'within industry standard.' It was not within our spec. We rejected the batch, and they redid it at their cost. Now every flange contract includes facing dimensions, MTRs, and marking requirements. The risk was a leak at pressure. The upside of cheaper flanges was maybe a few hundred dollars. That trade never made sense.
What separates precision machined components from 'close enough'?
Consistency. A single part can hit the print and still be a bad component if the next 500 don’t. I look for process capability, not just inspection data. Ask whether they can provide Cpk (process capability index, i.e., how consistently the process hits the spec) for critical dimensions. For low-volume work, FAI and in-process checks may be enough. For higher volume, SPC matters. I’m not a metallurgist, so I can’t speak to heat-treat grain structure. What I can tell you from a quality role is this: if the vendor only shows final inspection and no in-process plan, you’re buying hope. Precision machined components live or die on repeatability, not one good sample.
Are brass hose nipple connectors as simple as they look?
No. They are small, but they carry fluid, pressure, and sometimes vibration. I check alloy, thread type, thread engagement, barb dimensions, and whether the finish is compatible with the application. Lead-free brass is not optional for potable water or many regulated markets. Ask for RoHS and REACH statements if relevant. For a brass hose nipple connector, a small thread concentricity issue can cause a leak that shows up after assembly, not at receiving. One supplier sent parts with a decorative plating (which, honestly, caused more adhesion problems than it solved). We switched to bare machined brass with a defined surface finish and leak-tested samples. The unit price went up. The warranty claims went down. That’s the trade I’ll take.
What is the difference between aluminum CNC cutting and aluminum CNC machining?
People use the terms loosely. Aluminum CNC cutting often means profiling sheet or plate—sawing, routing, waterjet, laser—then maybe secondary operations. Aluminum CNC machining usually means milling and turning to create 3D features, holes, threads, and tight tolerances. If your part is a flat bracket, cutting may be enough. If it has pockets, bores, and a sealing face, you need machining. The quality question changes with the process. Cutting can leave heat-affected zones or edge dross. Machining leaves tool marks, burrs, and residual stress. Let me rephrase that: don’t ask 'which is better?' Ask 'which process produces the features I actually need, and how will you inspect them?'
Why does a washing machine Y splitter fail quality checks?
Usually at the threads or the seal. A washing machine Y splitter looks like a commodity, but a leak in a laundry room is expensive. I check inlet/outlet thread gauging, barb or compression fit, body material, and internal flow path. If it uses brass, I want alloy and lead compliance. If it uses plastic, I want UV and pressure ratings. The forgotten check is cross-threading. A thread that is 'almost' right can pass a visual check and fail after a few on/off cycles. We now require a thread gauge check and a low-pressure leak test on sample lots. The defect rate is boring now. That’s the goal. Boring quality is good quality.
Which documentation should I require before approving first delivery?
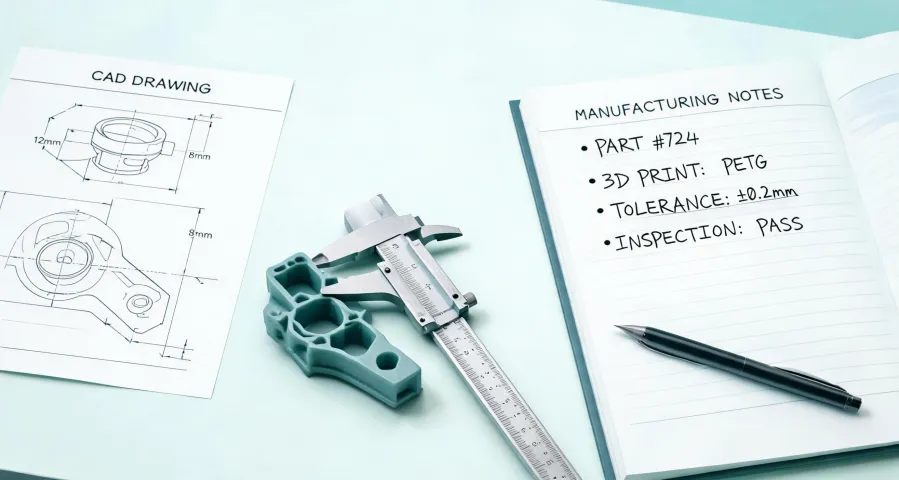
Start with a first article inspection report (FAIR), material certs or MTRs, certificate of conformance (CoC), and any required compliance statements. For flanges, reference ASME B16.5 and the material spec. For machined parts, include the drawing revision, GD&T, and critical dimensions. For brass connectors, add RoHS/REACH if applicable. If your industry requires PPAP, build that into the timeline. As of January 2025, many digital manufacturing platforms make documentation upload easier, but the burden is still on you to review it. I use Fictiv for quoting and order visibility, then I run my own incoming inspection. The platform helps with speed. It does not replace the quality plan.
What is the one question most buyers forget to ask?
What happens when something is out of spec? Anyone can quote a good part. The real supplier shows up when the part is wrong. Ask about their rework policy, response time, root-cause process, and who pays for expedited replacement. I once approved a vendor because their samples were excellent. Then the first production lot had a dimension that drifted. The sales rep disappeared for two days. The worst case was a full redo at $3,500. The best case was a quick sort and rework. The expected value said stay, but the downside felt catastrophic. Even after choosing them, I kept second-guessing. What if the next lot drifted too? We added a pre-shipment inspection clause. That fixed the relationship. The lesson: quality is not just the part. It is the recovery plan.
Reference points I use: ASME B16.5 for pipe flange dimensions; ASTM A105/A350 for carbon steel forgings; ISO 9001:2015 for quality management; RoHS and REACH for restricted substances. Verify current revisions and your customer-specific requirements before finalizing a PO.